Featured Modular Healthcare & Medical Building Systems
Precision-engineered, rapid-deploy modular medical space solutions designed for global disaster response, hospital expansions, remote clinical camps, and public health projects.
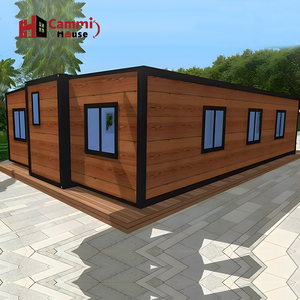
- HEPA H14 Negative Air Cascade
- Antibacterial HPL Wall Panels
- ISO 14644 Cleanroom Ready
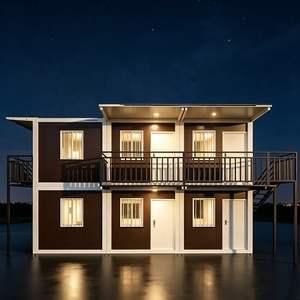
- Multi-Tier Structural Frame
- Integrated Medical Gas Trunking
- CE EN 1090 Structural Steel
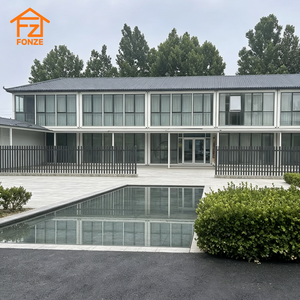
- Fireproof Rockwool Core (A1)
- Rapid 2-Hour Frame Erection
- Acoustic Rating 42 dB
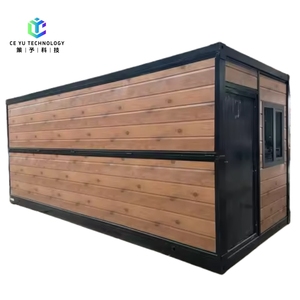
- 10-Minute Hydraulic Expansion
- Compact Sea-Container Footprint
- Pre-Wired Medical Power Grid

- BSL-2 / BSL-3 Safety Layout
- Seamless Epoxy Anti-Static Floor
- Vibration-Damped Instrument Bays
- Radiological Lead Shielding Option
- Laminar Laminar Flow Ceiling
- Hermetic Sliding Doors
- Thermal U-Value 0.21 W/m²K
- High-Traffic PVC Flooring
- Integrated HVAC Ducting
- Plug-and-Play Solar Integration
- Water Treatment Micro-Plant
- Heavy-Duty Galvanized Steel Frame
Future Healthcare Procurement Trends: The Strategic Shift to Modular Infrastructure (2025–2035)
The global healthcare construction sector is undergoing a structural paradigm shift. Traditional brick-and-mortar hospital construction, plagued by multi-year schedules, soaring material overheads, labor shortages, and high carbon footprints, is increasingly failing to meet the agility demands of modern healthcare administrators, humanitarian agencies, and municipal public health departments. In response, industrialized modular healthcare facility manufacturing has emerged as the global benchmark for capital-efficient, high-compliance clinical infrastructure.
Chinese modular building manufacturers have spearheaded this transition by combining world-class metallurgy, automated cold-formed thin-walled steel fabrication, and stringent cleanroom HVAC engineering. Today, top China modular healthcare building manufacturers do not merely offer temporary container shelters—they engineer permanent, expandable, and smart medical complexes that conform to WHO emergency hospital standards, ISO 14644 cleanroom classes, EN 1090 structural steel codes, and international building codes (IBC).
Information Gain Key Takeaway: Modern modular healthcare buildings reduce project delivery timelines by up to 70% while guaranteeing controlled cleanroom indoor air quality (IAQ) and seismic resiliency up to Richter Scale 8.0, making off-site industrialized construction the preferred choice for healthcare B2B procurement officers worldwide.
Key Engineering Drivers Accelerating Global Adoption
Rapid Deployment & Speed to Commission
Off-site volumetric manufacturing runs concurrently with on-site foundation work. Complete 200-bed field hospitals can be installed, sanitized, and commissioned within 14 to 21 days from port arrival.
Negative Pressure & Bio-Containment
Factory-integrated HVAC pressure cascades (-15Pa to -30Pa) with HEPA H14 filtration ensure zero cross-contamination between infectious disease wards, ICU bays, and clean doctor corridors.
Structural Longevity & Corrosion Resistance
Heavy-duty hot-dip galvanized steel frames (zinc coating ≥ 275g/m²) combined with fluorocarbon PVDF steel skin panels guarantee a 30 to 50-year structural life, even in extreme coastal or tropical environments.
Technical Specifications & Metallurgy Standardizations
Understanding the exact bill of materials (BOM) and mechanical parameters is critical for international hospital procurement teams. Below is the engineering matrix implemented across our standardized and custom modular healthcare modules:
| Structural / Mechanical Component | Technical Specification & Standard | Clinical & Operational Advantage |
|---|---|---|
| Primary Load-Bearing Chassis | Q235B / Q345B Cold-Formed Galvanized Steel Profiles (4.0mm - 6.0mm thickness) | Seismic resistance up to Grade 8 (Richter Scale); resists wind loads up to 210 km/h. |
| Wall Enclosure System | 50mm - 100mm PIR / High-Density Rockwool (120kg/m³) Sandwich Panels | Class A1 fire-rating; thermal conductivity U ≤ 0.21 W/m²K; high sound attenuation (STC 45). |
| Internal Surface Finish | Antibacterial HPL (High-Pressure Laminate) / PVDF Coated Galvanized Sheet | Seamless, non-porous surfaces resistant to aggressive chemical disinfectants (chlorine, H2O2). |
| Cleanroom Floor System | 18mm Fiber Cement Board + 2.0mm Homogeneous Conductive PVC Membrane | Anti-static, non-slip, rolled-up cove base wall joints eliminating bacteriological traps. |
| HVAC & Air Purification | Dedicated AHU with Primary G4, Medium F8, and Terminal HEPA H14 Filters | Filters 99.995% of airborne pathogens ≥ 0.3 µm; achieves ISO Class 5 to Class 8 air purity. |
| Medical Utility Integration | Factory-embedded conduits for O2, Vacuum, N2O, and Cat6A Shielded Data | Plug-and-play connection at site; reduces mechanical, electrical, and plumbing (MEP) labor by 80%. |
Manufacturing Superiority: Why Procurement Leaders Source from China
China's industrial ecosystem offers an unmatched supply chain synthesis for prefabricated health modules. By locating raw steel sourcing, precision roll-forming, HVAC manufacturing, medical gas equipment, and cleanroom wall production within unified industrial clusters, leading Chinese manufacturers achieve cost efficiencies and quality consistency unattainable in regional off-site yards.
Enterprise Quality Management (E-E-A-T)
Our manufacturing operations operate under a fully accredited ISO 9001:2015 Quality Management System, ISO 14001 Environmental System, and ISO 45001 Occupational Health Standards. Structural steel elements are CE certified according to EN 1090-1 / EN 1090-2 (Execution Class EXC2), providing European and global engineering consultants with absolute compliance security.
Every modular unit undergoes rigid factory acceptance testing (FAT), including 100% water tightness testing under pressurized spray nozzles, electrical insulation dielectric testing, and cleanroom air leakage rate verification prior to flat-pack or volumetric export packaging.
Optimized Logistics & Flat-Pack Architecture
Logistics costs frequently hinder international modular procurement. Our proprietary Flat-Pack Modular Healthcare Container System allows four complete 20ft medical-grade modules to be bundled into a standard ISO 20ft High-Cube shipping frame (4-in-1 SOC bundle).
This innovation slashes ocean freight costs by up to 75% compared to pre-assembled volumetric containers, enabling cost-effective bulk shipments to remote ports across Africa, South America, Southeast Asia, and the Middle East.
Comparative Analysis: Traditional Hospital vs. China Modular Medical Systems
To assist procurement committees in capital expenditure (CAPEX) vs. operational expenditure (OPEX) evaluations, the table below contrasts conventional healthcare construction against modular facility building systems:
| Evaluation Parameter | Traditional On-Site Hospital Construction | Module-T China Modular Medical Building |
|---|---|---|
| Construction Schedule | 24 – 48 Months (High delay risk) | 3 – 8 Weeks Factory Build; 7-14 Days On-Site Erection |
| Cost Predictability | Frequent 15%-30% budget overruns due to weather/labor | Fixed turnkey contract pricing; zero material wastage overhead |
| Quality Control | Variable on-site craftsmanship under harsh weather | Automated CNC factory assembly under controlled ISO standards |
| Scalability & Relocation | Permanent, non-expandable without major demolition | 100% Demountable, stackable (up to 3 stories), and fully relocatable |
| Environmental Impact | High carbon emissions, extensive noise, dust, and landfill waste | 80% reduced site carbon footprint; recyclable steel frames |
Frequently Asked Questions (FAQ) for Global B2B Buyers
The cost of modular healthcare facilities typically ranges between €250 and €650 per square meter, depending on the internal clinical grade requirements. Standard administrative offices or triage cabins sit at the lower price bound, whereas complex isolation wards, PCR laboratories, and cleanroom operating theaters requiring negative pressure HVAC, lead shielding, and medical gas piping reach the higher tier. Flat-pack shipping significantly lowers landed costs compared to fully built volumetric units.
Yes. Our modular medical facilities are structural-engineered according to Eurocodes (EN 1993 for steel structures), American ASCE 7 structural design criteria, and WHO technical guidelines for emergency medical facilities. Our engineering department works directly with your local structural engineers of record to supply detailed calculation books, CAD shop drawings, and BIM models to ensure smooth local permitting approvals.
Once foundation footings or flat concrete slabs are prepared, a trained assembly crew of 12 personnel equipped with a light mobile crane can assemble, interlock, and weather-seal a 100-bed modular facility (comprising approximately 30 to 40 flat pack container units) in 7 to 10 working days. Complete MEP connection, HVAC testing, and clinical sterilization add approximately 5 days prior to patient admission.
Negative pressure modules utilize sealed air-tight sandwich panel joints and automatic hermetic doors combined with an automated Air Handling Unit (AHU). The AHU exhausts slightly more air volume than it supplies, maintaining a negative room pressure differential between -15 Pa and -30 Pa relative to adjacent corridors. All exhaust air is passed through a high-efficiency HEPA H14 filter and UV-C germicidal irradiation chamber before discharge, eliminating pathogen leakage.
Absolutley. We engineer modules specifically for arctic cold (-40°C) using 100mm Polyisocyanurate (PIR) core insulation and floor heating mats, as well as desert environments (+50°C) utilizing solar-reflective PVDF roof coatings, double-glazed low-E argon windows, and tropicalized high-capacity HVAC chillers.