Featured Modular Oilfield & Remote Camp Accommodations
Select from our ISO 9001:2015 and CE-certified modular container series engineered for extreme remote operational zones, desert climates, sub-zero energy fields, and heavy industry deployment.
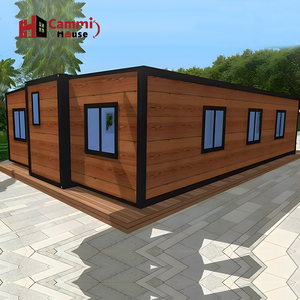
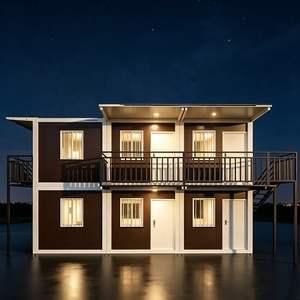
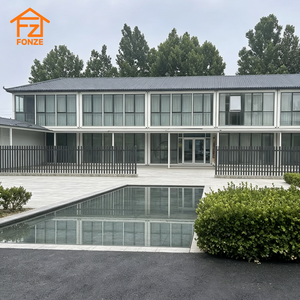
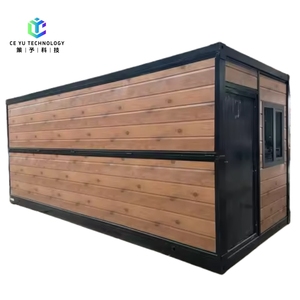
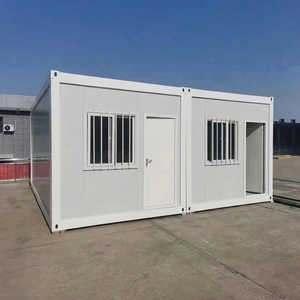
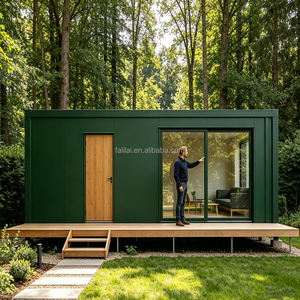
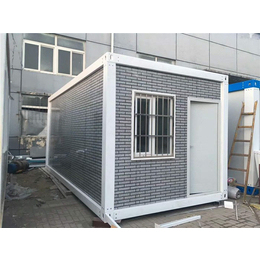
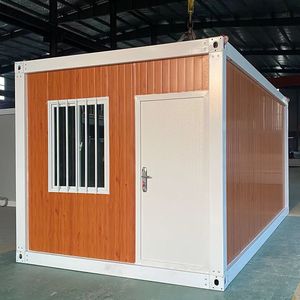
Engineering Specifications for Remote Oilfield & Energy Camp Construction
Deploying remote workforce housing in upstream oil & gas fields, offshore landing sites, and heavy mining infrastructure projects demands rigorous structural integrity, exceptional thermal efficiency, and complete environmental containment. As a premier Chinese manufacturing exporter, our engineering frameworks integrate high-yield cold-formed galvanized light gauge steel profiles (Q235B / S235JR and Q355B / S355JR structural grade steel) with advanced polyurethane (PUR), polyisocyanurate (PIR), or high-density Mineral Rockwool sandwich panels.
Information Gain Metric: Standardized remote camps utilizing our 4-in-1 flat-pack shipping structure reduce international freight volume by up to 75% compared to pre-assembled rigid volumetric units, fitting up to 4 complete 20ft modular cabins into a single 40ft High Cube sea container.
Whether navigating ambient operational temperatures of +55°C in the Middle East and North Africa (MENA) region or facing -40°C sub-zero environments in Northern Eurasia and North America, structural performance must comply with rigorous international standards. Our modular systems undergo comprehensive FEA (Finite Element Analysis) stress modeling to withstand extreme climatic variables, including wind loads up to 180 km/h (Category 5 hurricane compliance) and seismic ground acceleration matching Zone 8 standards (PGA > 0.3g).
Hot-Dip Galvanized Frames
Minimum 180g/m² to 275g/m² zinc coating, offering C3-C5 high-corrosion classification per ISO 12944 for coastal and desert saline environments.
Thermal & Acoustic Barrier
Wall thickness options from 60mm to 150mm PIR/Rockwool cores providing thermal transmittance (U-value) down to 0.18 W/m²K and sound reduction up to 42 dB.
Fire Safety Compliance
Class A non-combustible Rockwool panels achieving EI60 to EI120 fire resistance rating, ensuring strict compliance with EN 13501-1 and NFPA 101 safety codes.
Structural Comparison Table: Modular Building Systems for Remote Oilfield Projects
| Structural Parameter | Flat-Pack Container Units | Expandable Modular Cabins | Light Steel Prefab Buildings |
|---|---|---|---|
| Assembly Speed | 2–3 hours / 2 workers | 15–30 mins / 3 workers | 15–20 m² / worker / day |
| Logistics Efficiency | 4 units per 40ft HQ container | 2 units per 40ft HQ container | 150–200 m² floor space per 40ft HQ |
| Structural Lifespan | 20–25+ Years | 15–20 Years | 30–50 Years (Permanent) |
| Stackability & Layout | Up to 3 stories stacked | Single story or ground level | 1–2 stories steel frame |
| Best Operational Intent | Rapid deployment, multi-move oil camps | Emergency housing, quick setup command post | Central mess halls, long-term operational bases |
Manufacturer Capabilities, E-E-A-T Compliance & Factory QA Assurance
As a vertically integrated original equipment manufacturer (OEM) and leading Chinese exporter, our manufacturing infrastructure operates over 80,000 m² of modern production facilities with automated CNC cold-roll forming lines, laser cutting stations, and robotically welded structural frame assemblies. Our production management strict adherence to ISO 9001:2015 Quality Management Systems and CE marking under EN 1090-1 / EN 1090-2 (Execution Class EXC2 for Structural Steelwork) guarantees that every unit leaving our factory gate satisfies rigorous international procurement audits.
For international procurement teams operating under EPC (Engineering, Procurement, and Construction) contracts, regulatory verification and full material traceability are essential. Every structural column, corner fitting, roof beam, and insulated panel is batch-tracked with mill test certificates (MTC per EN 10204 3.1), guaranteeing structural steel tensile strength, anti-corrosion layer thickness, and fire barrier performance test compliance.
Factory Testing Protocol: Prior to export dispatch, units undergo rigorous water-tightness jet testing (under 0.2 MPa spray pressure), floor deflection testing (designed for 2.5 kN/m² live load), and electrical insulation testing in accordance with IEC 60364 international electrical safety standards.
Bespoke Architectural Customization
Fully tailored floor plans ranging from single-bed VIP manager cabins and 4-person worker dormitories to integrated sanitary modules, commercial kitchens, medical clinics, and laundry facilities.
End-to-End Global Logistics
Exporters serving 120+ countries with complete CIF/DDP delivery logistics, specialized protective packaging for ocean transit, and localized customs compliance assistance.
Turnkey On-Site Field Support
Provision of detailed 3D step-by-step assembly manuals, high-definition installation videos, and on-site engineering supervision for large-scale camp construction.
Future Procurement & Technological Trends in Remote Modular Camps
The global oilfield camp accommodation market is undergoing a rapid evolution driven by ESG (Environmental, Social, and Governance) mandates, strict workforce safety regulations, and digital transformation in remote asset management. High-performance modular camp procurement is shifting away from basic temporary shelters toward zero-carbon, intelligent, and highly comfortable living environments.
1. ESG Integration and Zero-Carbon Microgrid Compatibility
Modern remote energy camps are increasingly integrated with hybrid off-grid power generation systems. Forward-thinking Chinese factories are pre-engineering flat-pack modular units with integrated rooftop solar PV bracket systems, energy storage batteries (BESS), and smart microgrid interfaces. Combined with low-E energy-efficient glazing, smart LED motion lighting, and heat recovery ventilation (HRV) units, modular camp power consumption can be reduced by up to 35-45% compared to conventional remote accommodation units.
2. Positive Pressure Air Filtration & H2S Gas Mitigation
For upstream oil & gas fields operating near high-sulfur sour gas reserves or heavy dust desert conditions, living quarters require positive pressure HVAC air handling systems equipped with HEPA and activated carbon filtration matrices. This technology prevents the infiltration of toxic gases (such as Hydrogen Sulfide / H2S) and fine particulate dust (PM2.5 / PM10), safeguarding crew health and complying with international OHSAS 18001 / ISO 45001 occupational safety frameworks.
3. Circular Economy & Multi-Cycle Modular Reuse
Procurement teams are prioritizing structural modularity that supports multiple redeployment cycles. Flat-pack modular container units feature fully demountable structural steel frames designed for over 10 relocation cycles without structural degradation. Fast disassembly, containerized transport packaging, and standardized interchangeable wall panels significantly reduce capital expenditures (CAPEX) across sequential project phases.
4. Smart Camp IoT & Building Automation Integration
Next-generation remote camps incorporate central IoT control networks for monitoring real-time energy usage, water consumption, fire alarm status, and indoor environmental quality (IEQ). Factory-installed conduit pathways and embedded smart sensors allow camp managers to remotely optimize heating/cooling loads and manage predictive maintenance schedules across multi-building living quarters.
Frequently Asked Questions (B2B Procurement & Engineering)
Detailed technical responses addressing common procurement, structural engineering, logistics, and compliance inquiries from EPC contractors and energy sector purchasers.
How do Chinese modular accommodation factories guarantee anti-corrosion longevity in harsh desert/coastal oilfield sites?
Our structural steel frames undergo a multi-stage surface treatment process: initial shot blasting to Sa 2.5 standard, followed by hot-dip galvanization (180g/m² to 275g/m² zinc mass), and finishing with a 100-120 micron electrostatic powder coating or marine-grade epoxy paint system. This provides superior resistance against salt spray, atmospheric humidity, and high UV radiation, meeting C4/C5 corrosion classifications under ISO 12944 with a design life exceeding 25 years.
What is the standard production lead time for a 500-man turnkey oilfield accommodation camp?
For a standard 500-man camp complex—comprising sleeping quarters, ablution blocks, dining facilities, recreation halls, and administrative offices (approx. 120-150 container units)—the factory manufacturing cycle is typically 20 to 30 calendar days. Combined with automated roll-forming and pre-wiring assembly lines, our dual manufacturing plants can output up to 1,200 standard container units per month to meet urgent project mobilization schedules.
What foundation prep is required for installing flat-pack modular camps in remote desert regions?
Flat-pack modular container units can be positioned on point concrete pads, strip footings, compacted gravel beds with concrete sleepers, or ground screw anchor systems. For multi-story configurations (2 to 3 levels), a perimeter reinforced concrete beam foundation is recommended to ensure uniform load distribution and prevent differential settlement across desert sands or permafrost soils.
Are electrical and plumbing systems pre-installed according to destination country electrical codes?
Yes. Ceiling panels come pre-wired from the factory with concealed conduit runs, junction boxes, LED lighting, and distribution boards compliant with IEC, BS 7671, UL, or AS/NZS electrical standards. Plumbing fixtures, PPR water supply lines, and PVC waste pipes are fully integrated into sanitary modules, requiring only simple external quick-connect couplings during field setup.
What container loading options optimize ocean freight cost for bulk orders?
Our proprietary flat-pack design packages 4 individual 20ft container cabins into an ISO-certified SOC (Shipper Owned Container) bundle with identical dimensions to a standard 20ft intermodal container. Alternatively, up to 4 complete flat-pack units fit loosely inside a standard 40ft High Cube container, lowering per-unit sea transport costs by 75% compared to shipping rigid fully assembled volumetric structures.
Accelerate Your Remote Camp Procurement
Connect directly with our senior structural engineering team and global export managers. Receive turnkey camp layouts, detailed technical proposals, structural calculation reports, and factory-direct pricing within 24 hours.
Send an Inquiry